Project Challenge
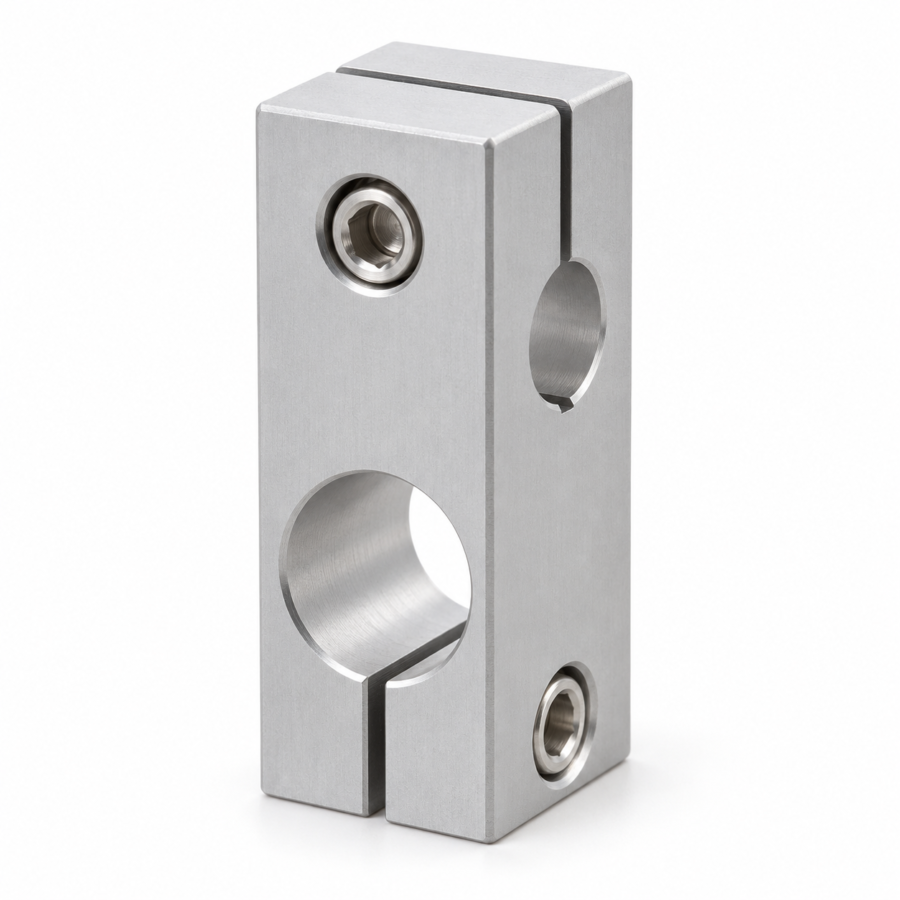
The clamp must hold the bore and split slot in the correct relationship while keeping recessed fastener pockets accessible and the two clamping faces stable.
Our Solution
We plan the bore, split slot and pocket sequence around stable datums, control material removal and finish the clamping faces after the main geometry is established.
Quality Check
Inspection can cover bore size, slot width, pocket depth, hole position, parallelism, clamping-face alignment and burr-free edges.
Part Overview
A split clamp block holds a shaft or cylindrical element while keeping the bore, split slot and fastener pockets aligned. This reference focuses on the compact rectangular form, clean bore, narrow split opening and controlled mounting features that are common in automation and equipment assemblies.
Manufacturing Approach
We establish the bore and primary faces as the datum system, then machine the split slot and recessed fastener pockets from controlled references. The sequence balances material removal around the bore and leaves the clamping faces stable for final sizing, deburring and surface treatment.
Quality Assurance
Inspection can cover bore diameter, slot width, pocket depth, hole position, parallelism, edge condition and clamping-face alignment. Final requirements, sampling and inspection records are agreed from the approved drawing before release.
Custom Clamp Block CNC Machining
Send your clamp block drawing, shaft diameter, material, quantity and finish. We will review the datums and return a practical machining and quotation plan.